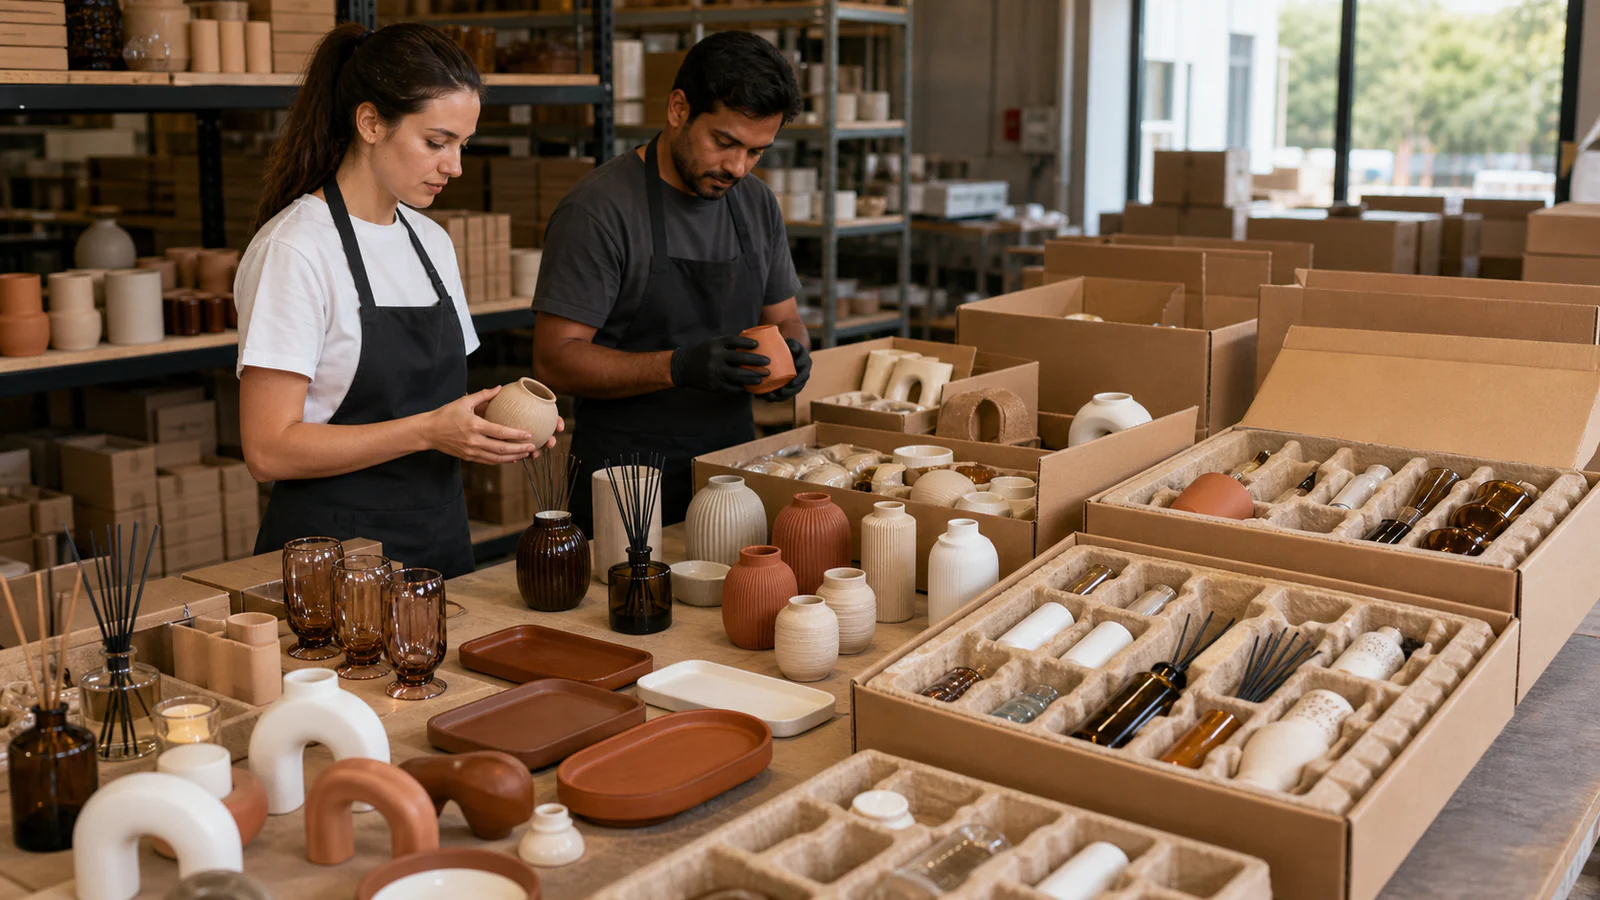
A buyer can submit an assortment with enough total units to look substantial and still receive a refusal on several lines. The issue is not the order total. One finish may miss a coating batch, one printed box may miss its packaging run, and one fragile shape may leave an incomplete master carton. Adding those units together does not make the underlying inputs interchangeable.
A mixed SKU home decor order therefore needs two views at the same time. The commercial view asks whether the range is broad enough for the market. The production view asks which lines genuinely share a material, process, finish, pack and release route. MOQ control happens where those two views meet.
The practical rule is simple: approve the order from the SKU upward, not from the purchase-order total downward. Every line must belong to a feasible production group, a defined packaging hierarchy, an identifiable carton and a released shipment plan.
Expose the total-order illusion before requesting price
“Twenty-four SKUs in one order” says nothing about whether those SKUs can be produced or packed together. Count the constraints that cannot be pooled.
| Apparent order condition | Hidden line-level failure | Required buyer decision |
|---|---|---|
| The grand total is above the supplier’s headline minimum | Quantities are split across unrelated materials or processes | Confirm the minimum at SKU, input-group and process-group level |
| Several colours use the same shape | Each colour needs a separate finish batch or approval | Decide which colours can share preparation and which remain separate |
| All items use branded packaging | Box sizes, inserts or print methods are not common | Use a packaging family or keep a stock-pack fallback |
| Carton count is sufficient overall | One SKU leaves a partial carton or mixed residual | Define carton multiples and the rule for approved mixed cartons |
| Goods can be sent to one consolidation point | Lines are not released at the same time or under one packing record | Set arrival, inspection, carton-data and loading gates |
Do not solve every failure by increasing every quantity. First identify whether the constraint belongs to the product, shared input, process, packaging or shipment layer. For the underlying effects of material, finish and packing choices, consult LANBORUI’s guide to wholesale home decor minimums; the method here turns those separate constraints into one mixed order.
Split MOQ into five control layers
MOQ is not a single field copied across a spreadsheet. A line can pass one layer and fail the next.
| Control layer | What may create the minimum | Mixed-SKU pooling question | Evidence to request |
|---|---|---|---|
| Product line | Form, component set, assembly route or model-specific setup | Can another SKU use the same product platform without changing the operation? | Product code, revision and approved bill of materials |
| Shared input | Material grade, colour preparation, coating or purchased component | Which SKUs consume the same controlled input? | Input-group code, purchase batch or preparation record |
| Process run | Printing, finishing, firing, moulding, assembly or test setup | Can the lines run under one method and acceptance reference? | Process-group code, setup basis and approved finish reference |
| Packaging family | Box structure, insert, print, label or barcode application | Can multiple SKUs use one pack platform while remaining identifiable? | Pack code, dieline/version, artwork and pack-out |
| Shipment unit | Inner pack, master carton, pallet or other logistic unit | Are quantities complete, labelled and ready for the same release? | Carton master, packing list and shipment-unit record |
The buyer should ask for a minimum and a rounding rule at each applicable layer. “MOQ 500” is incomplete unless the quotation says whether that number applies per design, per finish, per input group, per printed pack or per order.
Freeze one master SKU register before suppliers quote
Mixed orders become unstable when marketing names, factory codes and carton descriptions refer to the same item differently. Create one register and make every later file point back to it.
| Register field | Control purpose | Change that requires review |
|---|---|---|
| Buyer SKU and supplier item code | Connect commercial and production identities | Either code is added, reused or reassigned |
| Product revision and approved sample | Identify the physical reference | Shape, component, construction or approved sample changes |
| Material, colour and finish codes | Assign the line to shared-input and process groups | Any visible or technical input changes |
| Unit, inner-pack and master-carton quantities | Control order multiples and pack-out | Pack count, assortment or carton dimensions change |
| Packaging, artwork, barcode and label versions | Keep market-facing identity aligned | Artwork, identifier, language or retail pack changes |
| Ordered, released and packed quantities | Separate intention from approved output | Shortage, overage, rejection or substitution occurs |
Use the field structure in LANBORUI’s factory RFQ preparation article. In a mixed order, the register becomes the join key across the enquiry, sample record, purchase order, inspection result, carton master and packing list.
Distinguish shared inputs from look-alike inputs
Two items are not a group because they look similar in a catalogue. They share an MOQ only when the supplier confirms that the constrained input or operation is common.
Name the shared material, component, finish preparation or pack platform; the responsible process owner; each SKU’s allocation; the group minimum; and the rule for residual input or a departing SKU. Keep lines separate when substrates, firing conditions, coating chemistry, component interfaces, pack structures or acceptance references differ. A buyer-facing colour name such as “warm white” does not prove one factory batch.
Build an MOQ ledger that rolls upward from each SKU
The order becomes measurable when every line feeds the group that creates its constraint.
Use three linked quantities:
- Line quantity — the ordered quantity for one buyer SKU and revision.
- Group quantity — the sum of compatible line quantities assigned to one shared input, process or packaging family.
- Released quantity — the inspected and accepted quantity assigned to identified cartons.
A line is feasible only when its own non-poolable conditions pass and every group it depends on also passes. Do not use volume from an unrelated family to close a shortage. If a group fails, change the assortment, standardize the input, use a stock option, negotiate a documented exception or remove the line.
Form production families around compatibility, not merchandising themes
Retail buyers often build collections around colour stories, occasions or price points. Those are useful selling groups but may be poor production groups.
For order control, group SKUs by compatible material, process, finish preparation, component, pack platform, protection and release window. One merchandising collection can contain several production families, while one production family may support several merchandising stories. Keep both codes in the register instead of forcing one hierarchy to do both jobs.
Standardize only the variable that unlocks the order
Standardization can reduce fragmentation, but excessive standardization can erase the reason the range exists. Choose the smallest change that resolves the failed layer.
| Failed layer | Standardization option | What must remain controlled |
|---|---|---|
| Shared material or component | Use one approved grade, thickness or component platform | SKU-specific dimensions, function and approved appearance |
| Finish or colour preparation | Reduce finishes or assign more SKUs to one approved finish code | Colour tolerance, surface reference and line identity |
| Packaging print | Use one structural pack with SKU-specific labels | Correct product identification, language and barcode |
| Insert or protection | Develop a modular insert family where testing supports it | Fit, movement, surface contact and fragile-point protection |
| Carton multiple | Adjust line quantity to complete cartons | Ordered quantity approval and overage/shortage treatment |
| Release timing | Split the commercial launch or shipment where justified | Order records, cost allocation and receiving plan |
Record the commercial consequence before approving the change. A packaging platform may improve pooling but change shelf presentation. A shared finish may reduce range differentiation. A quantity round-up may create excess inventory. The mixed-order decision must show both the production benefit and the buyer-side cost.
Preserve SKU identity through the complete pack hierarchy
The product does not jump directly from “SKU” to “container.” It moves through nested units, and every handoff needs an identity and quantity.
The GS1 standards repository identifies the GS1 General Specifications as the foundational standard for identification keys, data attributes and barcodes. The current GS1 General Specifications define the SSCC for identifying a logistic unit. Apply GS1 identifiers only when the buyer, channel and trading partners require them; the operating principle is broader: every physical unit must be traceable to the records that describe its contents.
At each pack level, record the unit code/revision, contained SKUs and quantities, mixed or single-SKU status, required dimensions and weight, pack/label/identifier versions, destination allocation and release status.
Make the carton master the source for packing documents
The carton master should be built from actual approved pack-outs, not from estimated purchase-order arithmetic. Give every carton reference a contents rule.
For a single-SKU carton, the rule can identify the SKU, revision, quantity and carton sequence. For an approved mixed carton, it must list every contained SKU and quantity and use a conspicuous mixed-carton code. Residual quantities should never be placed into an unrecorded carton simply to close the shipment.
The official UN/CEFACT 2020–2021 activity report lists the Cross-Industry Export Packing List among its issued e-business standards. UNECE Recommendation 18 notes that a packing list supplements the commercial invoice when numerous items ship or when package quantities, weight or contents vary. That is exactly why a mixed order needs carton-level data before the final document is issued.
Reconcile four totals before release: ordered, accepted, packed and documented. A difference needs an approved cause, owner and disposition.
Release consolidation by gates rather than arrival date
Arrival at a warehouse or consolidation point is not shipment approval. A line can be physically present while its inspection, labels or carton data remain open.
| Release gate | Required evidence | Hold condition |
|---|---|---|
| Product gate | Correct SKU/revision, approved reference and accepted quantity | Wrong version, open defect or unapproved substitution |
| Pack gate | Approved pack-out, protection, label and identifier | Incomplete inner pack, wrong artwork or missing barcode record |
| Carton gate | Carton reference, contents, count, dimensions, weight and marks | Unidentified residual, mixed carton without contents list or count mismatch |
| Document gate | PO, inspection, carton master, invoice and packing-list reconciliation | Totals or descriptions do not agree |
| Load gate | Released cartons, compatible handling, loading plan and dispatch authority | Open hold, unsafe combination or unapproved loading change |
The LANBORUI quality-control route provides the wider inspection context. Mixed-SKU release adds one requirement: the inspection result must reconcile to a particular SKU revision and particular cartons, not only to a supplier-level pass status.
Protect fragile families when the load is assembled
Consolidation can create risks that do not appear in individual carton approval: incompatible weights, unstable stacks, crush risk, moisture exposure, protrusions or voids that allow movement.
The IMO/ILO/UNECE CTU Code is a non-mandatory global code addressing the packing and securing of cargo transport units across sea and land. It does not replace applicable regulations. Use its principle at the planning stage: the party assembling the load needs the actual packages, weights, dimensions, handling constraints and securing method—not merely the purchase-order total.
For a home decor assortment, keep heavy cartons away from crush-sensitive ones; separate surfaces that may scratch, stain or transfer; record orientation and stacking limits; hold cartons whose dimensions or weights differ from the approved record; and reapprove the plan when cartons, quantities or the transport unit change.
ISO 780:2015 specifies graphical symbols for handling and storage instructions on distribution packages and says they should be used only when necessary. Symbols support handling; they do not replace a tested pack, clear carton data or a load plan.
Check regulated wood packaging before dispatch
If raw-wood pallets, crates or dunnage are used, treat them as controlled shipment inputs. The IPPC’s ISPM 15 covers raw-wood packaging and identifies certain processed-wood exemptions. Confirm the destination rule, material, treatment/marking status, responsible provider and inspection evidence; a mark on one pallet does not establish the status of separate dunnage.
Run one assortment-release gate before the final order
The last decision should reveal every dependency that can still fragment the order.
- Can every SKU be identified? If not, stop and complete the register.
- Does every line pass its non-poolable minimum? If not, change or remove that line.
- Does every shared group clear its actual constrained input or process? If not, regroup, standardize or use a documented alternative.
- Do unit, inner-pack and carton multiples reconcile? If not, resolve residuals before confirming quantity.
- Can accepted units become identifiable released cartons? If not, hold packing and documentation.
- Can released cartons form a safe, documented shipment? If not, revise the release window or load plan.
Only then should the buyer treat the assortment as one order.
Frequently asked questions about mixed SKU home decor orders
Can different home decor categories share one MOQ?
Only when they genuinely share the input or operation creating the minimum. Items in one merchandising collection may still use different materials, processes, finishes or packaging. Require the supplier to name the pooled group, its minimum and the allocation by SKU.
What should an importer check before reducing quantity per SKU?
Check the non-poolable product minimum, shared-input group, process run, packaging family, carton multiple and release timing. A lower line quantity works only when the failed layer is resolved and the supplier confirms the basis in writing.
Is a mixed carton acceptable for a wholesale order?
It can be acceptable when the buyer and receiver approve it. Use a unique carton reference, complete contents list, visible mixed-carton identification and agreed label, inspection and receiving rules. Never hide residual units in an undocumented carton.
Should every SKU have its own barcode?
Requirements depend on the buyer’s channel and trading partners. Where GTINs or other barcodes are required, control their allocation and packaging level. A shipment-unit identifier does not replace the item identifiers or contents record inside it.
Can goods from different factories be consolidated into one shipment?
Yes, but arrival is not release. Each line should pass product, pack, carton and document gates before entering the load plan. Name who reconciles the records and who may stop loading.
Which details change the cost or risk of a mixed-SKU order?
SKU count, input and process groups, finish fragmentation, pack versions, carton multiples, inspections, delivery windows, consolidation handling, dimensions, weight and fragile-load controls can all matter. Request each dependency instead of one unexplained surcharge.
Convert the assortment into a factory-ready order brief
Send the supplier one register that connects buyer SKU, factory code, revision, group memberships, ordered quantity, pack hierarchy, carton multiple, required identifiers, destination and release evidence. Ask the supplier to return every failed layer, permitted pooling rule and rounding consequence by line.
For a mixed wholesale program, review the importer and wholesaler solution, factory and export capability, decorative homeware collection, home fragrance and incense collection and catalog request route. When the register is ready, send the mixed-order brief to LANBORUI for a factory quotation route.
Sources and editorial notes
- GS1 — Standards repository
- GS1 — General Specifications
- UN/CEFACT — Report of the twenty-seventh session
- UNECE Recommendation 18 — Facilitation Measures Related to International Trade Procedures
- IMO/ILO/UNECE — Code of Practice for Packing of Cargo Transport Units
- ISO 780:2015 — Distribution packaging graphical symbols
- IPPC — ISPM 15, Regulation of wood packaging material in international trade
Editorial disclosure: the MOQ ledger, pack hierarchy and assortment-release gate are original LANBORUI editorial tools. They are not a customer purchase order, supplier quotation, live MOQ promise, legal opinion, inspection record, packing list, logistics label, factory commitment or completed shipment. The article explains an order-control method; actual feasibility, quantities, processes, packaging, identifiers, costs, timing, inspection scope and transport requirements depend on the selected products, suppliers, destination, buyer channel and agreed specifications.