Record-template scope: Use this article to structure inspection evidence and release records from pre-production through shipment. For the broader quality plan, packaging validation and carton-control method, use the quality control and export packing guide.
A final inspection is not a time machine. If the approved finish was unclear, the first piece was never authorized or mixed SKUs entered one inspection lot, opening cartons before shipment only reveals decisions that should have been controlled earlier.
This home decor quality inspection checklist gives importers and wholesalers five gates: pre-production readiness, first-piece authorization, in-process control, approved-pack verification and pre-shipment acceptance. It does not promise zero defects, prescribe universal AQL values or replace product-specific testing.
Treat inspection as a release system, not a final-day event
Inspection should answer one question: may this order move to the next controlled state? A pass is meaningful only when the reference, lot, method, sample and decision authority are explicit.
| Gate | Decision being made | Minimum output | Stop condition |
|---|---|---|---|
| Pre-production | May materials and instructions enter production? | Released specification, approved references and control plan | Conflicting revision, missing limit or unapproved material |
| First piece | May the process continue beyond setup? | Signed first-piece record tied to SKU and revision | Visible or measured result falls outside the agreed reference |
| In process | Is the process remaining stable enough to continue? | Dated checks, issue counts, containment and correction record | Recurring failure, uncontrolled rework or mixed status |
| Packing | May inspected units enter the approved packing route? | Pack standard, label/mark checks and quantity reconciliation | Wrong protection, assortment, label or carton identity |
| Pre-shipment | May the defined lot be released? | Sampling instruction, inspection report and disposition | Failed acceptance rule, open critical issue or incomplete correction |
The LANBORUI quality-control route can support the commercial discussion, but the order still needs its own written specification and buyer-approved limits.
Freeze one approval file before opening the lot
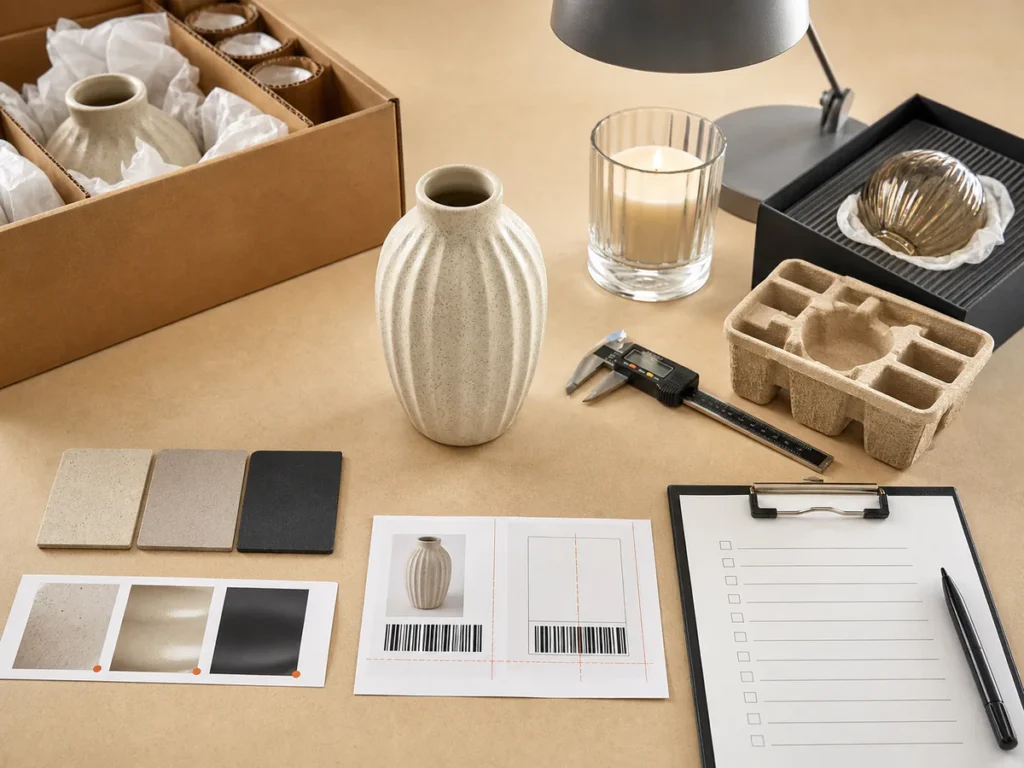
Inspectors cannot judge “good quality” consistently. Give them a controlled file that identifies what to check, how to check it and which evidence has authority when two references disagree.
| Control-file field | What to record | Why it changes the decision |
|---|---|---|
| Product identity | Buyer item number, supplier SKU, description and approved revision | Prevents one style or revision being judged against another |
| Visual reference | Approved sample ID, dated finish panel and controlled photographs | Defines colour, texture, sheen and workmanship boundaries |
| Measurable characteristic | Nominal value, tolerance, unit, method and measuring tool | Replaces subjective language with a reproducible check |
| Functional requirement | Test setup, conditioning, duration and pass/fail result where applicable | Makes function checks repeatable and scope-limited |
| Compliance input | Market, applicable requirement, model/material scope and owner | Separates regulatory evidence from routine appearance inspection |
| Packing reference | Unit protection, inner pack, assortment, labels, barcode and carton mark revision | Connects product acceptance to the exact shipping configuration |
| Conflict rule | Order of precedence among signed specification, approved sample and later change record | Stops an inspector from choosing whichever reference is easiest |
| Authority | Who may approve a change, concession, rework or release | Keeps commercial pressure from becoming an undocumented acceptance |
Use one dated change log. Resolve any conflict between the sample and written specification before production. A sales-chat message should not silently revise a signed approval file. Before this order-control stage, use the supplier-shortlisting guide to structure candidate review.
Define the lot before choosing a sample
A sampling result applies only to its defined lot. Set the boundary before calculating a sample or opening cartons.
| Lot attribute | Acceptable definition | Warning sign |
|---|---|---|
| Product | One SKU or a documented homogeneous family | Unrelated shapes grouped to reduce sample work |
| Material and finish | Same controlled material, colour/finish code and process route | Matte, glazed, plated and painted versions mixed |
| Revision | Same approved specification and change status | Old and new artwork or construction in one lot |
| Production window | Traceable run, date range, line or subcontract route where relevant | Reworked and unreworked units mixed without identity |
| Packing state | Same retail pack, inner pack and carton configuration | Some units packed, some loose and some awaiting labels |
| Quantity | Count reconciled to production and packing records | Estimated quantity or unexplained shortage/overage |
Mixed cartons do not automatically form one meaningful lot. Build sub-lots when failure modes or process histories differ, then record how their results affect release.
Turn defect classes into observable rules
“Critical, major and minor” are not universal labels. The buyer should define them around foreseeable consequence, contractual requirement and order use, then provide examples for the exact product.
| Buyer-defined class | Decision question | Home decor example to define—not assume | Typical control response |
|---|---|---|---|
| Critical | Could the condition create an unacceptable safety, legal or prohibited-use risk? | Exposed sharp edge on an intended-use surface; required warning or traceability absent | Contain the lot and escalate under the buyer’s critical-defect rule |
| Major | Would the condition likely prevent intended use, sale, assembly or agreed presentation? | Unstable base, wrong dimension affecting fit, prominent finish mismatch or wrong retail identity | Count against the agreed major rule; investigate and correct |
| Minor | Is the condition a limited departure that does not impair intended use but falls outside the approved workmanship boundary? | Small, defined cosmetic variation outside the approved zone | Count against the agreed minor rule and monitor recurrence |
Photograph borderline examples and define permitted zones, viewing conditions and handling where relevant. Do not downgrade a safety or compliance concern because it appears once.
Gate 1: prove pre-production readiness
Pre-production control asks whether the planned process can make the approved item—not whether a meeting occurred.
Confirm:
- specification, sample, artwork, material and packing instructions share one revision;
- purchased materials and subcontracted finishes match the approved identity;
- special characteristics, product tests and compliance tasks have owners;
- measuring tools and fixtures suit the required range and decision;
- inspection records, hold areas and status labels are ready; and
- open deviations have owners, deadlines and consequences.
ISO’s explanation of ISO 9001 emphasizes process control, responsibilities, documented information and monitoring. It supports controlling inputs before release but does not certify this order.
For measured characteristics, record tool identity and control status. ISO 10012:2026 addresses confidence that measurement processes and equipment are fit for purpose. The approved specification—not the standard—creates the product tolerance.
Gate 2: authorize the first conforming piece
The first-piece gate converts the approval file into a production reference. Select it after normal setup using planned materials, tooling, finish and assembly—not a hand-finished sample.
Record:
- SKU, lot or run identifier, revision, date and responsible people;
- the characteristics checked and the method or visual condition used;
- actual measured or observed results;
- photographs tied to the record, including any controlled finish reference;
- every adjustment made after the first check; and
- the final authorization, hold or rejection decision.
If an adjustment changes a controlled feature, inspect a new piece and retain the failed record. First-piece authorization never removes in-process monitoring.
Gate 3: inspect while correction is still possible
Target in-process checks where variation enters: material, tool or finish change; subcontract return; restart; or repeated rework.
| Trigger | Focused check | Evidence | Escalation |
|---|---|---|---|
| New material or finish batch | Identity, colour/finish reference and affected dimensions/function | Batch link and comparison result | Hold affected output from the change point |
| Setup, tooling or mold change | First-piece characteristics and fit/assembly | New authorization record | Do not merge status with the earlier run |
| Process interval chosen by the control plan | High-risk visible, measured and functional features | Time-stamped result and quantity since last accepted check | Increase containment when the trend worsens |
| Defect or rework recurrence | Cause, affected window and effectiveness of correction | Defect count, disposition and recheck | Stop if boundaries cannot be traced |
| Subcontract process return | Identity, finish/process requirement and transport damage | Receipt and verification record | Segregate unverified return |
Do not invent a universal hourly frequency. Base it on stability, consequence, production speed, detection difficulty and correction time. Trend repeated defects even before a sample crosses an acceptance number.
Gate 4: verify packing against the approved pack
This gate verifies that accepted product enters the approved packing system. It does not design the packaging or prove distribution performance.
Verify:
- product identity across unit label, retail box, inner pack and carton mark;
- specified contact points, dividers, bags, caps and surface protection;
- clean, dry and complete product before enclosure;
- quantity, assortment, accessories and instructions at every pack level;
- barcode content and buyer-defined scan result where required;
- sealing, orientation, carton number, recorded weight and dimensions when specified; and
- separation of inspected, reworked, held and released units.
ASTM D4169-23e1 describes laboratory performance-test sequences for shipping units; it does not replace pack specifications or routine inspection. Package engineering needs a separate plan.
Gate 5: run pre-shipment acceptance on a ready lot
Do not sample a partial lot unless the instruction defines that scope. Agree the readiness state—production, packing, sealing and marking as relevant—before booking.
Give the inspector one sampling instruction:
| Instruction field | Required entry |
|---|---|
| Lot | SKU/sub-lot identity, quantity, revision, process/finish and packing state |
| Sampling scheme | Named standard/version or buyer-specific rule, inspection level and plan |
| Sample selection | How units and cartons are selected across the lot without supplier preselection |
| Defect classes | Order-specific critical, major and minor definitions with examples |
| Acceptance rule | Sample size and acceptance/rejection numbers for each class |
| Tests | Characteristic, method, tool/fixture, sample allocation and result format |
| Evidence | Required counts, photographs, measurements, carton distribution and document copies |
| Disposition | Who may release, hold, reject, rework, re-inspect or accept a concession |
Report what was available, selected, excluded and changed from the instruction. A “pass” without the lot, sample and acceptance rule is not auditable.
Use AQL without turning it into a quality promise
ISO 2859-1:2026 provides AQL-indexed schemes for lot-by-lot inspection. ISO 28590:2017 guides selection and use of the series. Use the purchased standard or qualified support; this article does not reproduce its tables.
Apply four controls:
- Choose the scheme for the inspection situation. Repeated lot-by-lot inspection and isolated lots are not the same problem. ISO 2859-2:2020 addresses isolated lots or short series using limiting quality, where switching rules are not applicable.
- Define the lot first. Do not merge unlike SKUs, finishes or process histories for convenience.
- Randomize selection across the lot. Supplier-presented “good samples” invalidate the decision logic.
- Keep the claim narrow. Acceptance sampling is a lot-disposition tool under a stated plan. It does not prove every unit is conforming, guarantee defect-free delivery or replace process control.
No single AQL value fits all home decor. Set the plan from buyer requirements, consequences, product use, process knowledge, contract and market obligations. Even a 100% check remains vulnerable to human or measurement error.
Match checks to the product’s failure modes
Build the checklist from credible use, display, retail and transport failures—not a generic template.
| Product family | High-value inspection focus | Method boundary |
|---|---|---|
| Ceramic or glass vases | Stability, dimensions/opening, cracks/chips, glaze/finish boundary, leakage only when intended to hold liquid | Define surface zones, lighting and leakage method; visual sampling cannot prove material composition |
| Metal candle holders | Stability, assembly, weld/edge finish, coating, dimensions and heat-use features defined by the product standard | Routine inspection does not replace applicable heat, fire or material testing |
| Decorative lights | Identity, assembly, visible workmanship, function and required markings/document scope | Electrical safety and market compliance require qualified product-specific assessment |
| Mirrors and frames | Dimensions, frame/joint condition, visible distortion boundary, hanging hardware identity and protection | Installation suitability depends on wall, hardware, load and instructions |
| Resin or mixed-material ornaments | Balance, assembly, attachment strength under a defined method, colour/finish and complete components | Do not infer chemical compliance from appearance |
| Incense or aroma accessories | Stability, fit, surface/edge condition, intended-use features and required warning/instruction identity | Heat, emissions or substance questions may require specialist tests outside routine inspection |
For U.S. products subject to a CPSC-enforced rule, the CPSC explains testing and General Certificate of Conformity responsibilities; not every decorative product requires a GCC. The EU General Product Safety Regulation summary describes the framework applying from 13 December 2024. Importers must identify exact product and market obligations with qualified support.
When laboratory competence matters, ISO/IEC 17025:2017 addresses competence, impartiality and consistent laboratory operation. Accreditation scope, method, sample identity and report limitations still need review.
Close nonconformities before shipment release
A failed check does not create a corrected lot. Trace the affected window and separate held from released product.
| Closure step | Required evidence | Release question |
|---|---|---|
| Observe and classify | SKU, unit/carton, defect class, photo or measurement and reference breached | What exactly failed? |
| Contain | Physical/status segregation and affected quantity or time window | What cannot move while the issue is open? |
| Correct and determine cause | Rework/sort instruction, cause analysis proportionate to recurrence and owner | Has the immediate condition and repeat mechanism been addressed? |
| Verify correction | Re-inspection method, new sample/100% scope where agreed and results | Does the corrected population meet the written rule? |
| Decide disposition | Release, rework again, reject, replace or buyer-authorized concession | Who has authority, and what residual condition is accepted? |
| Update the record | Final quantities, labels/status, shipment documents and lessons for the control plan | Can the shipment be reconstructed later? |
A concession names the nonconformity, quantity, lot, impact, validity and approver; it cannot waive a legal or safety obligation. After rework, define a new re-inspection population and rule.
Frequently asked questions about home decor quality inspection
When should a home decor order be inspected?
Use staged controls before production, at first piece, during risk-based process triggers, when packing begins and on the pre-shipment lot. Frequency depends on stability, consequence and correction time.
Does an AQL pass mean the shipment has no defects?
No. It means the sampled lot met the stated rule under the selected plan. Sampling does not examine every unit, guarantee defect-free delivery or prove compliance.
Can different home decor SKUs share one inspection lot?
Only under a defensible homogeneous definition. Different materials, finishes, revisions, process routes or packing states usually require sub-lots.
What information should an inspection report contain?
At minimum: order and SKU identity, lot definition and quantity, readiness state, sampling plan, selected cartons/units, defect definitions and counts, measurements/tests, photographs, packing checks, discrepancies, unavailable scope, corrective actions and authorized disposition.
Is a pre-shipment inspection enough for a first order?
Usually not for new materials, finishes, functions or packing. Late inspection detects defined problems but cannot recover time or prove earlier process control.
Who should approve a failed inspection or concession?
The contract and quality plan should name the buyer-authorized role. The inspector records evidence; the factory proposes correction; the authorized buyer decides the disposition.
Send one inspection control pack with the RFQ
Prepare one file containing product revisions, references, limits, tests, lot architecture, defect examples, sampling instructions, packing standard, report format and release authority.
Use the factory RFQ guide to connect that control pack to SKU quantities, market, delivery window and commercial terms. Review the broader quality and export-packing article for context, the customization route for controlled changes and the sourcing workflow for order-stage responsibilities.
When the specification and inspection pack are ready, request a LANBORUI factory quotation with the category, destination market, quantity by SKU, timing, packing direction and required inspection evidence. A quotation should confirm how the requested controls can be applied; it should not replace buyer approval.
Evidence and publication boundary
The evidence base combines LANBORUI’s live content inventory with official material on process control, measurement, acceptance sampling, laboratory competence, distribution testing and U.S./EU product-safety frameworks. Research was checked on 25 July 2026.
The gate map, defect model and corrective-action loop are original editorial tools. They are not LANBORUI factory records, customer evidence, defect statistics, laboratory results, certificates or performance claims. A named LANBORUI quality, production or packaging reviewer must confirm terminology and current capability before publication. The buyer remains responsible for order-specific acceptance rules and applicable legal, technical and market requirements.