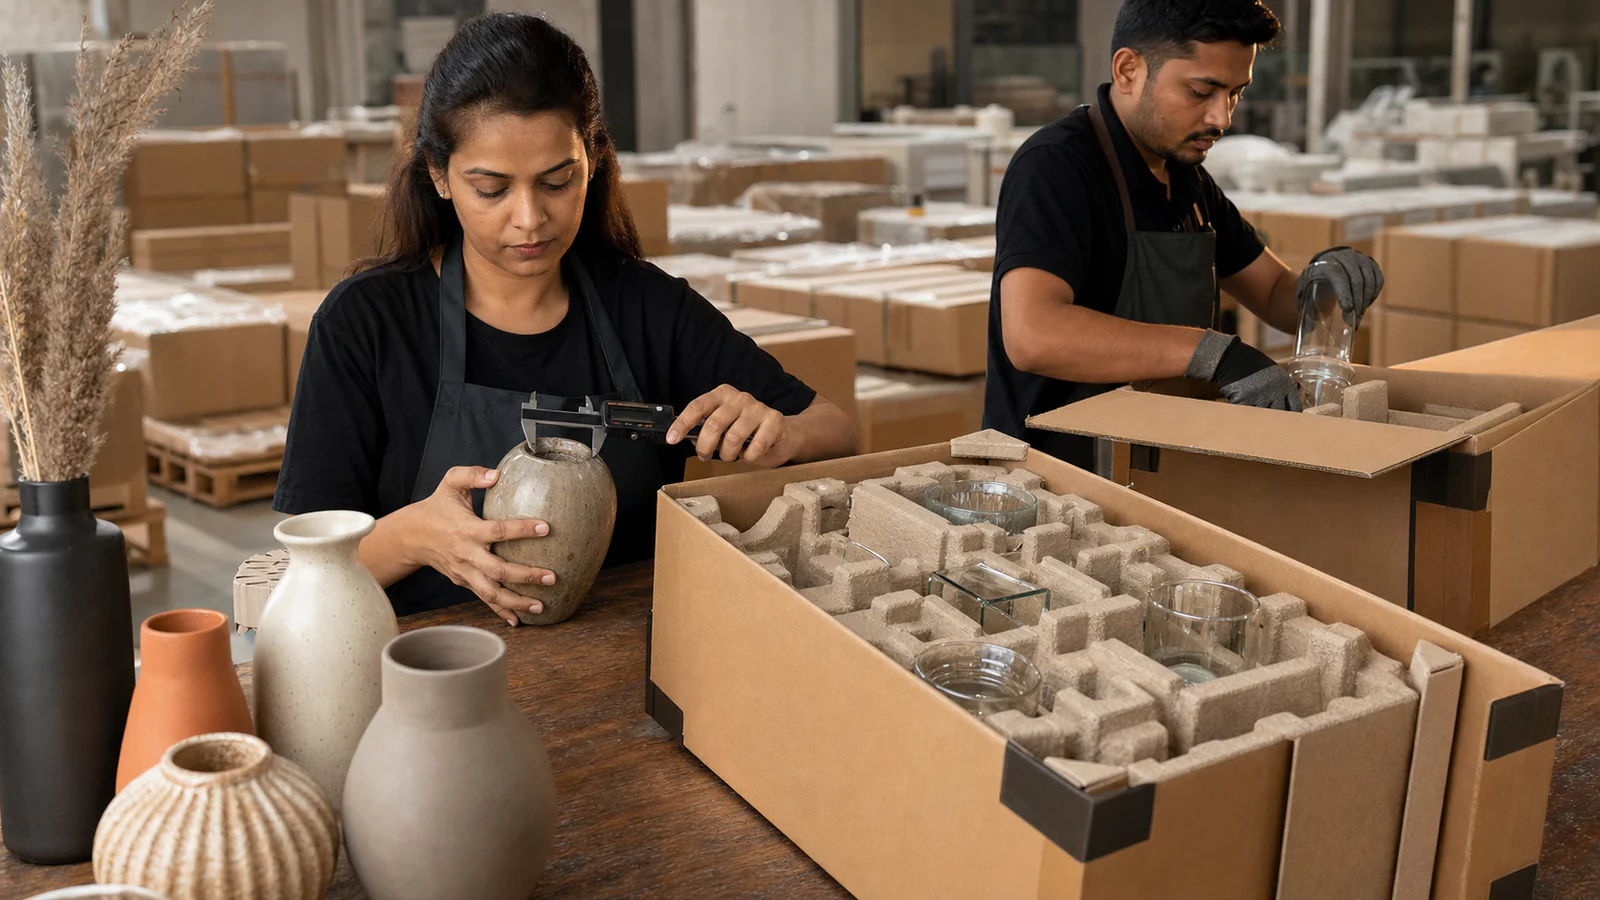
Quality control for wholesale home decor is not one final inspection performed after the cartons are closed. It is a connected system that begins with an approved product reference, follows the order through materials and production, and ends with evidence that the correct SKUs were packed for the agreed distribution route. This matters because decorative homeware combines visual expectations with practical risks: glaze variation, unstable bases, sharp edges, weak joints, fragile glass, scratched finishes, incorrect labels, mixed assortments and cartons that look acceptable until they are stacked or dropped.
This guide is for importers, wholesalers, retailers, hospitality buyers and private-label brands preparing a purchase order or inspection instruction. It explains how to build an order-specific quality plan, how to separate product conformity from sampling, and how to connect unit protection, master cartons, palletization and shipment records. It is not a universal inspection standard, laboratory test plan or legal opinion. The buyer must define the product, destination market and distribution route before selecting checks or acceptance rules.
The short answer: control the reference, the process and the release
A reliable home decor quality plan answers three questions. First, what exactly is the approved product and package? Second, which checks will detect the most likely failures while correction is still possible? Third, who has authority to stop, rework and release the shipment?
The strongest plan normally contains seven linked records:
- Controlled product specification: current SKU, dimensions, materials, finish, construction, function and tolerances.
- Approved reference: signed sample, limit sample, artwork proof, packaging sample or another clearly identified approval object.
- Defect classification: order-specific critical, major and minor defects with photographs or examples where practical.
- Inspection plan: lot definition, sampling method, checkpoints, measurements, tests and acceptance authority.
- Packing specification: unit protection, retail presentation, inner pack, master carton, assortment and pallet requirements.
- Execution evidence: incoming, in-process, final inspection and packing records tied to the SKU, order and date.
- Release record: final quantities, carton data, unresolved deviations, approved concessions and shipment decision.
A pass stamp without these connections is weak evidence. It may show that someone inspected something, but not that the inspected product matched the buyer’s approved revision or that the packed shipment remained the same after inspection.
Start with one controlled product and packaging specification
Inspection cannot compensate for an incomplete specification. If “cream ceramic vase” is the only reference, the inspector has no controlled basis for judging colour range, pinholes, glaze pooling, wobble, rim shape, dimensions or packing. The specification should identify the selected SKU and describe the characteristics that matter to sale, use and transport.
Product identity and revision
Use one SKU code, product name and revision ID across the RFQ, sample record, purchase order, packing instruction and inspection booking. If a colour, material or box changes, update the revision rather than sending an untracked message saying “use the latest version.” A practical revision record states what changed, who approved it, the date and whether price or delivery changed.
Measurable and visual requirements
Separate measurable requirements from visual approvals. Dimensions, weight, opening diameter, base flatness, wall thickness, component position and carton size may be measured. Glaze character, handmade variation, brushed-metal direction, antique treatment and colour range may require an approved sample or approved limit references. Avoid converting a visual expectation into an unrealistic numeric tolerance merely to fill a form.
Construction and intended use
Describe how the product is assembled and used. A decorative wall item needs hanging-point and fixing checks. A candle accessory may require heat-use review. A vase sold as watertight requires an agreed leakage check; a decorative vessel sold for dried flowers may not. A lamp, toy-like ornament or food-contact item can create requirements beyond ordinary non-electrical decor. Product labels do not decide the legal scope by themselves, so the importer should verify the intended use and applicable market rules.
Packaging as part of the approved reference
Approve the retail pack, protective inserts, labels, barcode position, inner quantity, master carton and shipping marks with the product. A beautiful product can still become an unacceptable delivery if a corrugated divider rubs a finish, a label covers a design feature, or mixed SKUs are placed in the wrong carton.
Classify defects before the inspection is booked
Generic defect lists create arguments because the same issue can have different commercial significance on different products. Define defect classes around safety, saleability, function, appearance and packaging.
Critical defects
A critical defect is one that can create an unacceptable safety, legal or serious use risk under the agreed scope. Examples may include an exposed sharp edge, insecure electrical part, unstable hanging hardware, prohibited material, incorrect mandatory warning or a structural failure likely to injure a user. Do not copy these examples into every order. The applicable critical list must follow the product and market.
Major defects
A major defect can make the item unsaleable, unfit for its intended use or materially different from the approved reference. Examples can include severe colour mismatch, leakage where watertightness was agreed, a rocking base, a loose metal joint, a visible crack, wrong component, unreadable barcode, missing retail pack or inadequate protection that has already caused damage.
Minor defects
A minor defect is a departure that does not materially reduce intended use but affects finish or workmanship. Small surface marks outside a defined viewing area or modest handmade variation may fall here. The category should reflect the sales channel: a luxury gift box and a rustic handmade planter do not share the same visual acceptance boundary.
Use limit samples for subjective variation
Where “acceptable” cannot be captured in words, approve upper and lower visual limits. Photograph the limits under consistent light and retain physical samples when the finish is difficult to reproduce on screen. The inspection instruction should state which reference governs if photographs, written notes and physical samples disagree.
Choose inspection timing by correction opportunity
The purpose of a checkpoint is to make a decision while the relevant problem can still be corrected. Adding more inspections after production is complete does not replace earlier process control.
Incoming material and component checks
Check high-risk inputs before they are consumed: glass thickness or colour, ceramic body or glaze reference, metal grade or coating sample, resin formulation reference, magnets, hanging hardware, candle cups, fragrance-contact components, labels, printed boxes and protective inserts. Record supplier or batch identity only to the level needed for the order’s risk and traceability plan.
First-piece or pre-production confirmation
Confirm the first production output against the controlled reference before the full run accelerates. This is especially useful for new moulds, complex decoration, colour matching, printed packaging, mixed materials or assembly fixtures. A pre-production sample approved months earlier may not represent the actual bulk materials, so identify whether the first-piece check is an additional gate.
In-process inspection
Inspect when enough units exist to reveal process behaviour but enough time remains for containment. For ceramics, this may involve formed bodies, fired ware, glazing or decoration stages. For metal decor, inspect formed parts, welds, surface preparation, coating and assembly. For gift sets, check component availability, assortment and packaging before every carton is sealed.
Pre-shipment inspection
A final inspection should use finished, packed goods from a defined lot and compare them with the current specification and approval set. Record the production completion percentage, available quantity, carton locations and how samples were selected. If the goods were not sufficiently complete or accessible, the report should say so rather than implying a full final inspection.
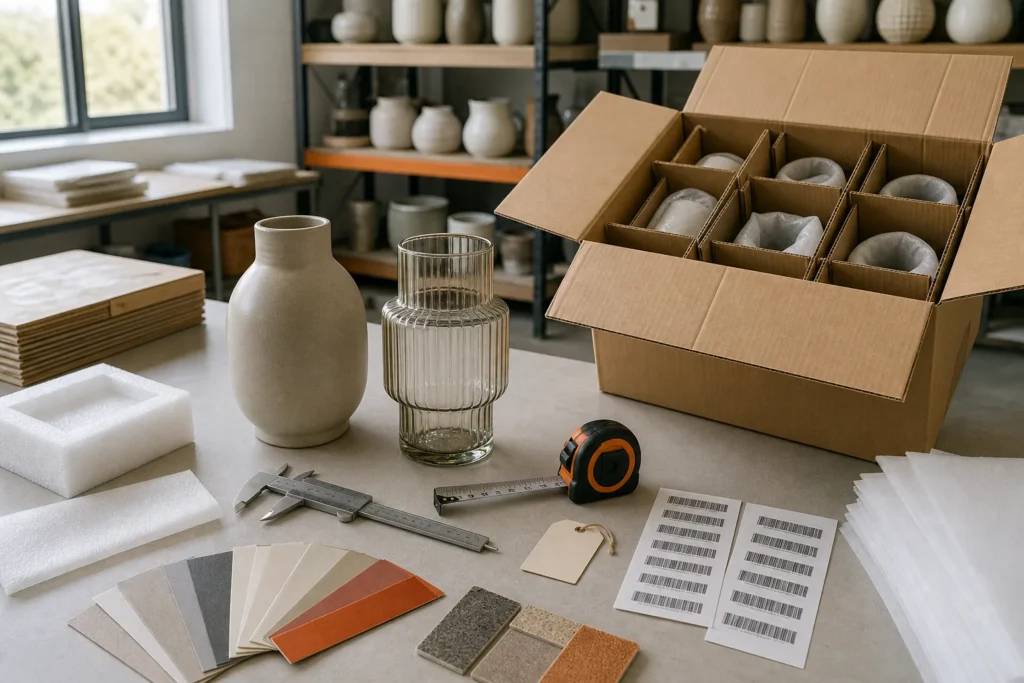
Use sampling as a decision method, not a quality promise
Acceptance sampling helps a buyer make a lot-level decision without examining every piece. It does not prove that every unit is conforming, and an “AQL pass” is not a certificate of product safety or market compliance.
ISO 2859-1:2026 defines AQL-indexed sampling schemes for lot-by-lot inspection by attributes. The buyer and supplier still need to agree the lot, inspection level, defect classes, AQL values or other acceptance limits, switching rules where relevant, and the action following a failed result. A third-party inspection company may propose a plan, but the commercial parties must understand and approve it.
Define the lot
A lot should represent units produced under sufficiently consistent conditions for the selected sampling approach. Do not combine unrelated SKUs, production periods or factories into one convenient number if their risks differ. Record quantity by SKU and colour, plus the cartons available at inspection.
Keep critical decisions separate
Safety-relevant or legally required characteristics may need zero acceptance in the sample, dedicated testing, document review or a different control method. Do not assume that the same AQL used for cosmetic marks is suitable for sharp edges, electrical safety or mandatory information.
Specify what happens after failure
A failed inspection should trigger a controlled decision: hold, sort, rework, replace, re-inspect, accept under a documented concession or cancel under the commercial agreement. “The factory will improve” is not a disposition. Record affected quantity, containment, root cause where needed, corrective action, owner and verification.
Build product-specific checks for common home decor families
One factory checklist cannot cover every material and use. Start with the product’s likely failure modes and add only checks that answer a real acceptance question.
| Product family | Useful order-specific checks | Common packing risk |
|---|---|---|
| Ceramic vases and planters | Dimensions, base stability, cracks, glaze range, pinholes, rim condition, drainage feature and leakage if promised | Rim impact, body-to-body contact, weak divider, moisture retained before packing |
| Glass vases and candleware | Chips, cracks, stress points, wall and base condition, edge finish, colour and accessory fit | Insufficient suspension space, glass contact, loose candle cup, carton compression |
| Metal decor and stands | Welds, joint alignment, stability, coating adhesion reference, scratches, burrs, hardware count and assembly | Abrasion between parts, protrusions puncturing cartons, moisture affecting finish |
| Resin or composite decor | Mould detail, deformation, voids, surface finish, colour, odour where relevant and base protection | Point loading, surface transfer, deformation under heat or stacking |
| Mixed-material gift sets | Correct assortment, component compatibility, insert fit, orientation, labels and replacement-piece control | Components moving inside the set, finish transfer, missing pieces, wrong SKU combination |
| Wall and hanging decor | Fixing position, attachment strength plan, balance, sharp projections, supplied hardware and instructions | Hardware rubbing the face, bending, puncture and incorrect accessory bag |
If the product includes electrical parts, flame or heat exposure, children’s use, food contact, chemicals or another regulated characteristic, create a separate compliance and test plan. Do not generalize a decorative-vase inspection to those categories.
Design export packing as a four-level system
Export protection should be designed from the product outward and from the distribution route backward. The correct pack for palletized wholesale delivery can differ from the pack for parcel fulfilment or store-ready mixed cartons.
Level 1: product-surface protection
Protect visible surfaces, edges, openings, protrusions and loose components without creating new damage. Soft wraps can mark some finishes; printed paper can transfer ink; plastic can trap moisture; tape can leave residue. Test the actual material against the actual finish rather than approving a generic packing name.
Level 2: unit or retail pack
The unit pack controls movement and may carry brand, barcode, warning, importer or product information. Approve the insert orientation, opening experience and product-to-pack clearance. A private-label box is both a presentation item and a technical component of the transport system.
Level 3: inner and master carton
Define units per inner and master carton, divider structure, void control, carton board or performance requirement, closure method, gross weight, dimensions and assortment. Carton strength must be evaluated in the context of weight, stacking, humidity, handling and shipment duration. A supplier’s familiar carton may not fit a heavier product or a new distribution channel.
Level 4: pallet or container load
Define pallet pattern, maximum height, corner protection, stretch wrap, straps where used, overhang limits and carton orientation. For floor-loaded containers, confirm how cartons are blocked, separated and protected from doors, walls or concentrated loads. The final plan should allow counting and inspection without destroying the load.
Validate the product-and-package combination
Packaging tests should reflect the shipment route and the decision the buyer needs to make. A simple drop screen can help compare two insert designs, but it does not automatically predict performance across every route.
The International Safe Transit Association’s test-procedure overview distinguishes integrity screening, partial simulation, general simulation and enhanced simulation. ISTA also emphasizes understanding the actual distribution environment when selecting and interpreting a procedure. Choose a qualified test route when the product value, fragility, sales channel or customer requirement justifies it, and define product damage and package-degradation criteria before testing.
- Use screening tests to compare designs early, not to make unsupported universal claims.
- Test the packaged product, not an empty carton or a product wrapped differently from production.
- Record specimen identity, pack revision, test sequence, conditions, result and post-test inspection.
- Reassess when product weight, dimensions, materials, pack quantity or distribution route changes.
Control moisture, abrasion and mixed-SKU movement
Breakage is visible, but surface and moisture damage can create equally expensive claims. Allow products and coatings to reach the agreed condition before wrapping. Keep dirty or wet packing materials out of the line. Where humidity exposure is material, use an engineered moisture-control plan based on product, packaging, route and duration; do not add desiccant by habit without calculating need and controlling placement.
For mixed cartons, use a carton-level assortment record. A final total by SKU is not enough if receiving teams cannot identify which carton contains which item. Confirm that dividers remain stable when different shapes share one carton and that heavy items cannot migrate onto fragile ones.
Record carton data before shipment release
The packing record connects physical goods to freight planning, warehouse receiving and commercial documents. Capture:
- purchase order, SKU, description and revision;
- unit, inner and master-pack quantities;
- carton number or range and SKU assortment;
- carton dimensions, net weight and gross weight;
- shipping marks, barcode and destination-label revision;
- pallet quantity, dimensions and gross weight where applicable;
- final packed quantity and variance from the order;
- inspection status, concession reference and release owner.
If solid-wood pallets, crates or dunnage are used, confirm the destination’s phytosanitary requirements. The International Plant Protection Convention explains that ISPM 15 provides a harmonized approach for wood packaging material in international trade and uses a recognized mark for material treated according to the standard. Processed wood products and other exemptions must be assessed against the applicable rules; a logo printed by an unapproved party is not evidence of compliant treatment.
Separate product inspection, packaging validation and compliance evidence
These three controls answer different questions:
- Product inspection: does the sampled production lot match the approved order criteria?
- Packaging validation: does the defined product-and-package combination withstand the selected handling or test conditions?
- Compliance evidence: have the responsible parties identified and met the requirements for the product, intended use and destination market?
A passed factory inspection does not create a laboratory report. A package test does not prove chemical, electrical or labeling compliance. A management-system certificate does not prove that one shipment matches its specification. Buyers should keep the evidence separate while linking each record to the same SKU and revision.
For EU-bound products, official EU product-compliance guidance states that importers must ensure imported products conform to applicable EU law and verify relevant documentation, labels, traceability and instructions. Requirements vary by product. The importer should obtain qualified advice instead of asking a supplier for a vague certificate saying that all home decor is compliant.
Use a controlled response when inspection fails
Do not release a failed lot because shipment space is booked. First contain the affected goods and identify whether the issue is isolated, systematic or caused by the reference itself.
- Describe: SKU, lot, quantity, defect, location and evidence.
- Contain: stop packing or shipment and identify potentially affected goods.
- Decide disposition: sort, rework, replace, scrap, accept by written concession or another agreed action.
- Correct: change material, method, fixture, training, inspection or packing as supported by the cause.
- Verify: inspect corrected goods under a defined plan and update the record.
- Prevent recurrence: update the specification, limit sample, process control or packing instruction where needed.
If the buyer accepts a deviation, record the exact SKU, quantity and condition. A concession for one order should not silently become the new production standard.
Step-by-step quality and export-packing workflow
- Define the product and market. Confirm intended use, destination, channel and responsible importer.
- Freeze the approval set. Connect the product specification, physical or visual reference, artwork and pack revision.
- Map failure modes. List product, finish, assembly, label, assortment and transport risks.
- Set defect classes and checks. Define what is measured, visually compared, functionally checked or tested.
- Select checkpoints. Use incoming, first-piece, in-process and final inspection where each adds decision value.
- Approve the packing system. Confirm product protection, unit pack, master carton and pallet or container plan.
- Choose the sampling and test route. Record the lot, method, acceptance rules and action after failure.
- Inspect production and packed goods. Preserve dated evidence tied to SKU, order and revision.
- Close deviations. Record containment, corrective action, re-inspection and any buyer concession.
- Release against one shipment record. Match passed quantities, cartons, marks, weights and documents before handover.
Buyer checklist before approving shipment
- [ ] Current product, artwork and packing revisions match the purchase order.
- [ ] Approved samples and visual limits are available to production and inspection teams.
- [ ] Defect classes and product-specific checks are documented.
- [ ] Lot and sampling method are identified; critical checks are treated separately where necessary.
- [ ] Final inspection used sufficiently complete, accessible and packed goods.
- [ ] Failed findings have a documented disposition and verification.
- [ ] Unit protection and retail packaging match the approved production pack.
- [ ] Master-carton quantity, dimensions, weights and closure are recorded.
- [ ] Mixed-SKU assortment and carton numbering can be traced.
- [ ] Pallet or container loading requirements are confirmed.
- [ ] Wood packaging requirements are confirmed where solid wood is used.
- [ ] Product compliance, package validation and shipment inspection evidence are not being confused.
- [ ] Shipment release is signed by the person with agreed authority.
Questions buyers ask about home decor quality control
Is AQL the same as product quality?
No. AQL-indexed acceptance sampling is a method for making decisions about lots from samples. Product quality also depends on the specification, process controls, approved references, defect definitions and corrective-action system. A passing sample does not mean every unit is defect-free.
Should every order receive a third-party inspection?
Not automatically. The decision depends on product risk, supplier history, order value, internal capability and customer requirements. A new supplier, new product, corrective-action order or high-risk pack may justify more independent control. Stable repeat orders may use a different plan, but the change should be deliberate.
Can the factory perform the inspection?
Yes, factory inspection can be part of the system if the criteria, records and release authority are clear. The buyer may still use independent verification for selected orders or risks. The important issue is not the logo on the report but whether the person has access, competence, independence appropriate to the decision and authority to stop nonconforming goods.
How many cartons should be opened?
That depends on the lot, sampling plan, SKU mix, inspection level and specific risks. Do not use one fixed carton count for every order. The plan should also explain how cartons and units are selected so the sample is not limited to the easiest goods to reach.
Does a drop test prove that export packing is sufficient?
Not by itself. A drop test can screen or evaluate particular impact conditions. The relevant distribution environment may also involve vibration, compression, handling, humidity, pallet movement or parcel sorting. Select a test and acceptance criteria that match the product and route.
Who is responsible for product compliance?
Responsibilities depend on the market, product and commercial roles. Importers and brand owners often retain obligations that cannot be transferred by asking the factory for a certificate. Identify the applicable rules and responsible economic operators before finalizing labels, tests and documents.
Related sourcing guides
- Wholesale Home Decor Supplier Checklist: 25 Questions Before You Request a Quote
- Home Decor Manufacturer vs Trading Company: Which Sourcing Route Fits Your Order?
- How to Prepare a Clear RFQ for a China Home Decor Factory
- LANBORUI quality-control workflow
- Factory and export capability
Sources, method and limits
This guide combines factory-side order-control practice with public primary references: ISO 2859-1:2026 for lot-by-lot sampling by attributes, ISTA test-procedure categories and its guidance on selecting tests for the distribution environment, the IPPC guide to ISPM 15, official ICC Incoterms® 2020 information and EU product-compliance guidance. Standards and legal requirements change and may require paid documents or professional interpretation. Apply only the requirements relevant to the selected product, market, contract and shipment.